Below is a comprehensive breakdown of the key industries and suitable raw materials that rely on rotary drum granulator technology.
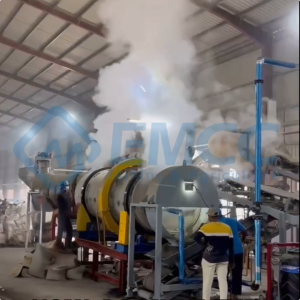
1. Compound & Chemical Fertilizer Industry
The commercial fertilizer sector represents the largest global application for rotary drum granulators. They are essential for producing high-grade, free-flowing commercial fertilizer pellets that withstand long-distance bulk shipping and mechanical broadcasting.
Key Suitable Materials:
-
NPK Compound Fertilizers: Balanced nitrogen-phosphorus-potassium formulations (e.g., NPK 15-15-15, 17-17-17, 20-10-10).
-
Urea-Based Blends: Formulations utilizing urea melt, ammonium nitrate, or ammonium sulfate.
-
Phosphate Fertilizers: Monoammonium Phosphate (MAP), Diammonium Phosphate (DAP), Single Superphosphate (SSP), and Triple Superphosphate (TSP).
-
Potash & Sulfur Fertilizers: Potassium chloride (KCl), potassium sulfate (K2SO4), and elemental sulfur granules.
Process Advantage: Rotary drums excel at steam granulation and slurry ammoniation. Injecting steam or liquid slurries into the rolling bed raises bed temperatures to 65 ℃ to 85 ℃, boosting salt solubility, building superior granule crushing strength ( ≥ 20 N), and lowering downstream drying fuel costs.
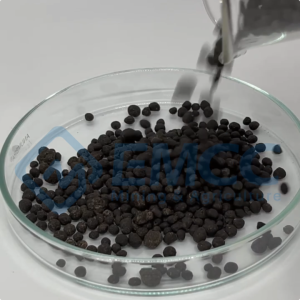
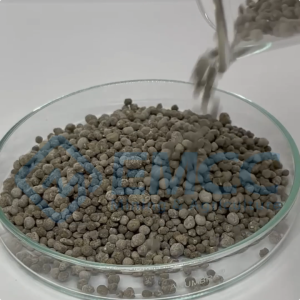
2. Organic & Bio-Organic Fertilizer Recycling
As agriculture shifts toward sustainable soil management, large-scale organic waste recycling facilities utilize heavy-duty drum granulators to process high-volume organic feedstocks.
Key Suitable Materials:
-
Livestock Manure Compost: Processed poultry manure, cow manure, and pig manure after pre-composting and moisture adjustment.
-
Agricultural Biomass & Residues: Crop straw ash, peat, humic acid, lignite, and biochar powders.
-
Bio-Organic Formulations: Organic bases blended with functional microbial inoculants, where controlled bed rolling prevents bacterial damage.
-
Industrial Organic Wastes: Monosodium glutamate (MSG) residue, spent grains, sugar mill filter cake (press mud), and alcohol slop (vinasse).
3. Mining, Metallurgy & Mineral Processing
In heavy mining and extractive metallurgy, fine mineral dusts must be agglomerated into green balls or stable granules before furnace smelting or heap leaching to ensure optimal gas permeability.
Key Suitable Materials:
-
Metallic Mineral Powders: Fine iron ore concentrates (for pelletizing plants), copper concentrates, manganese dust, and zinc oxide powders.
-
Industrial Minerals: Bentonite clay, kaolin, gypsum, bauxite, limestone powder, and fluorite fines.
-
Coal & Carbon: Fine coal dust, coke breeze, and activated carbon powders.
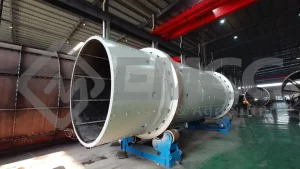
4. Environmental Protection & Solid Waste Management
Drum granulators provide an effective waste-to-resource solution by converting hazardous or difficult-to-handle industrial waste powders into manageable commercial materials or safe landfill aggregates.
Key Suitable Materials:
-
Fly Ash & Slag: Coal combustion fly ash from thermal power plants, steel slag fines, and blast furnace dust.
-
Municipal & Industrial Sludge: Dewatered sewage sludge and industrial wastewater sludge combined with solidifying agents.
-
Flue Gas Desulfurization (FGD) Gypsum: Synthetic gypsum produced from coal plant emissions, converted into soil amendments or construction pellets.
5. Chemical Processing & Building Materials
High-volume industrial chemical synthesis often demands granular forms to eliminate airborne dust hazards, improve storage bulk density, and optimize metering.
Key Suitable Materials:
-
Chemical Compounds: Sodium carbonate (soda ash), calcium chloride, titanium dioxide, detergent powders, and synthetic catalysts.
-
Building Material Aggregates: Lightweight expanded clay aggregates (LECA), ceramic raw materials, and cement raw meal powders.
Industry Applicability Summary
| Industry Sector | Primary Materials Processed | Core Equipment Benefits |
| Compound Fertilizers | NPK, Urea, MAP, DAP, Potash | Massive line capacity (10-30+ t/h); steam injection capability |
| Organic Fertilizers | Manure compost, humic acid, biochar | Handles sticky, fibrous organic feedstocks at scale |
| Mining & Metallurgy | Iron ore fines, bentonite, coal dust | High mechanical durability; creates dense green balls for furnaces |
| Environmental Recycling | Fly ash, FGD gypsum, industrial sludge | Converts dusty solid waste into eco-friendly building aggregates |
| Industrial Chemicals | Soda ash, detergent bases, titanium dioxide | Reduces dust hazards; improves powder flowability and handling |
Conclusion
The rotary drum granulator is the gold standard for high-capacity, continuous agglomeration. Whether processing high-nitrogen NPK fertilizers, recycling agricultural biomass, pelletizing iron ore fines, or stabilizing industrial fly ash, its ability to handle continuous heavy tonnage with low maintenance makes it an essential asset for modern industrial processing plants.